
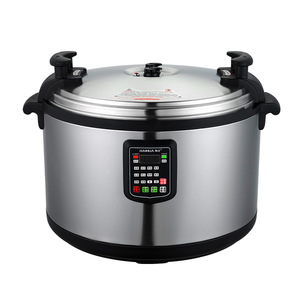
Commercial Large Capacity Electric Pressure Cooker
- Heavy-gauge Non-Stick Inner Tank
- Stainless Steel Commercial Housing
- Dual Safety Release Valve System
Engineered for global importers, B2B distributors, and private labels. Compliant with FDA 21 CFR 175.300, LFGB Section 30/31, RoHS, and CE standards.
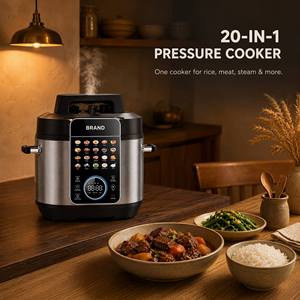
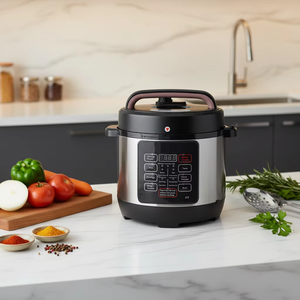
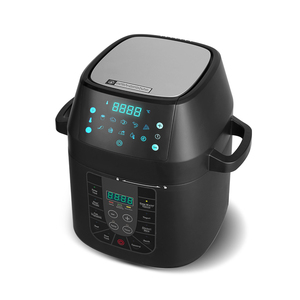
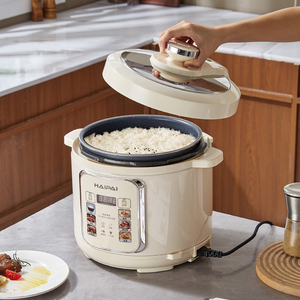
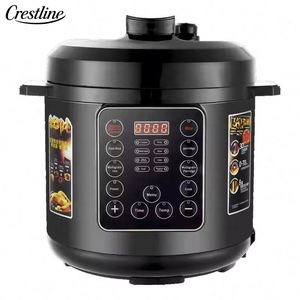
Combining legacy foundry craft with state-of-the-art robotic spray-coating lines and stringent international quality assurance protocols.
Navigating the global kitchenware supply chain requires more than simple vendor identification—it demands a deep alignment on metallurgical engineering, non-stick polymer science, thermal distribution physics, and international compliance frameworks. China’s non-stick cookware manufacturing landscape represents the world’s most advanced ecosystem for die-cast aluminum, heavy-gauge forged aluminum, tri-ply stainless steel, and smart electric pressure cooking systems. As a dominant global exporter and original equipment manufacturer (OEM), our integrated production facilities bridge high-volume automated manufacturing with rigorous quality control standards (ISO 9001:2015, BSCI, and ISO 14001 certified).
From initial mold tool drafting to final robotic automated spray coating in Class 10,000 cleanrooms, our manufacturing ecosystem provides global brand owners, chain hypermarkets, and institutional importers with direct engineering access. We specialize in producing non-stick frypans, deep kadhai sets, sauté pans, casserole sets, crepe tawas, multi-cooker inner vessels, and commercial electric pressure cookers engineered to withstand high thermal stress and intense mechanical wash cycles.
Information Gain Procurement Insight: The structural durability of non-stick cookware is fundamentally governed by the interface chemistry between the metallic substrate surface pretreatment (sandblasting grit roughness Ra 3.5–4.5 µm) and the primer coat anchor. High-performing China exporters utilize multi-stage automated tunnel shot-peening to maximize surface area before applying fluoropolymer or ceramic matrices.
A comprehensive comparative breakdown of non-stick cookware base metals, forming techniques, and multi-layer coating systems.
| Manufacturing Technology | Material Substrate Alloy | Wall Thickness Range | Coating System Options | Thermal Distribution Index | Target B2B Market Segment |
|---|---|---|---|---|---|
| Die-Cast Aluminum | ADC12 / A380 Aluminum Alloy | 4.5mm - 7.0mm Heavy Gauge | 3-Layer PTFE / Sol-Gel Ceramic | 9.8 / 10 (Superior) | High-End Culinary Brands & Professional Chef Lines |
| Forged Aluminum | 3003 / 4006 Pure Aluminum Sheet | 3.0mm - 4.5mm Medium-Heavy | Granite Marble Coating Matrix | 9.2 / 10 (High) | Retail Hypermarkets, Mid-to-High Department Stores |
| Stamped Aluminum | 1050 / 1100 Commercial Aluminum | 1.8mm - 2.5mm Light Gauge | 2-Layer Standard PTFE Fluoropolymer | 7.5 / 10 (Moderate) | Promotional Bundles, Mass E-Commerce, Value Sets |
| Tri-Ply Clad Stainless Steel | SS304 (Inside) + Alu Core + SS430 (Base) | 2.5mm - 3.2mm Clad Composite | Plasma-Sprayed Reinforced Non-Stick | 9.5 / 10 (Induction Optimized) | Commercial Hospitality, Hotel Supplies & Luxury Lines |
Utilizing high-molecular-weight Polytetrafluoroethylene (PTFE) modified with PFA (Perfluoroalkoxy) and FEP (Fluorinated Ethylene Propylene). Formulated as 3-layer systems (Primer, Mid-Coat with mineral reinforcement, and Topcoat) delivering over 45,000 cycles of MKT abrasion resistance under BS EN 12983-1 protocols. 100% PFOA-Free and GenX-Free compliant.
Engineered via room-temperature hydrolysis and low-temperature condensation polymerization of liquid silanes and metal alkoxides. Creates an inorganic silicon dioxide ($SiO_2$) matrix that resists thermal breakdown up to 450°C (842°F). Completely free of PFAS, PTFE, Lead, and Cadmium, matching strict eco-label green procurement mandates.
Electrochemical bath treatment converting surface aluminum into a glass-hard aluminum oxide ($Al_2O_3$) layer with hardness exceeding 400 HV (Vickers scale)—twice as hard as stainless steel. Provides an impervious base for non-stick topcoats while eliminating warping, thermal hotspot distortion, and metal utensil gouging.
Key technological transformations shaping brand positioning, regulatory compliance, and consumer purchasing intent across North American, European, and Asian markets.
Global regulatory pressure (including U.S. EPA mandates and EU REACH Annex XVII restrictions) is accelerating the complete phasing out of fluorinated compounds. Future-ready China factories are investing heavily in 4th-generation Sol-Gel ceramic technologies and diamond-reinforced silica coatings that achieve non-stick contact angles ($\theta > 105^\circ$) comparable to classic PTFE while retaining 100% toxic-free certification.
Traditional sprayed-mesh induction dots are rapidly being replaced by full-coverage, impact-bonded SS430 magnetic stainless steel plates applied under 2,500-ton hydraulic forging presses. This eliminates bottom warping during high-wattage induction cooking, maximizes thermal energy transfer efficiency by up to 35%, and ensures zero plate-separation failures in high-heat commercial usage.
ESG compliance is shifting cookware manufacturing toward 80%+ certified Post-Consumer Recycled Aluminum (PCR 3003/6061 alloys). Modern Chinese exporters utilize closed-loop smelting facilities certified under ISO 14021 environmental labeling, reducing the embodied carbon footprint per cookware unit by up to 78% compared to primary virgin aluminum extraction.
With urbanization and smaller modern living spaces, modular cookware sets featuring click-lock detachable Bakelite or stainless steel handles are growing at a CAGR of 11.4%. These systems require precision-engineered die-cast side bosses and mechanical stress testing to ensure the locking mechanism withstands over 15,000 cycle load tests (holding up to 10kg weight at full extension).
How top China cookware exporters verify structural integrity, chemical safety, and coating longevity before container loading.
Every batch of aluminum ingots or sheets undergoes optical emission spectrometer (OES) chemical analysis to confirm alloy purity (ensuring zero heavy metal contamination like Lead, Cadmium, or Arsenic). Substrate grain density is verified under microscopic cross-section to eliminate internal porosity before die-casting or stamping.
Destructive laboratory testing follows rigorous international standards:
• Cross-Hatch Cut Test (ASTM D3359 / ISO 2409): 1mm grid scoring followed by 3M tape pull to ensure Class 5B zero-flaking adhesion.
• Mechanical Scourer & Steel Wool Test: Reciprocating pad testing under 1.5kg load for 20,000+ continuous cycles.
• Salt Spray Corrosion (ASTM B117): 5% NaCl continuous fog exposure for 72+ hours to verify anti-corrosion barrier integrity.
Finished cookware units are heated repeatedly to 260°C (500°F) on high-wattage burners and immediately submerged into 15°C cold water. This thermal shock cycle is repeated 50 times sequentially to ensure zero delamination, micro-crazing, or substrate base deformation occurs under extreme cooking conditions.
Final outward goods inspections adhere to ISO 2859-1 sampling plans. Visual surface defects (blisters, pinholes, color variance $\Delta E < 0.5$, scratch marks) are audited under AQL 1.0 Major / 2.5 Minor thresholds alongside handle torque strength testing (minimum 8 Nm rotation torque resistance).
Streamlining private-label manufacturing from custom mold prototyping to DDP door-to-door delivery.
Equipped with 5-axis CNC machining centers, 3D laser scanners, and mold tooling shops. We reduce custom sample turnarounds to just 7–10 days for new pan silhouettes, specialized lids, or custom ergonomic handle designs.
100% Pantone color-matching accuracy for outer heat-resistant silicone polyester paints and inner granite coatings. Full custom packaging options including 5-ply color display boxes, protective drop-test mailer packaging, and eco-friendly zero-plastic inserts.
Every shipment is accompanied by batch-specific test reports issued by accredited third-party laboratories (SGS, TÜV Rheinland, Intertek, Bureau Veritas) confirming full compliance with FDA, LFGB, DGCCRF, EU Directive 1935/2004, and California Prop 65.
Direct answers to critical technical, financial, and logistical questions encountered during China OEM/ODM factory sourcing.
Standard OEM production MOQs start at 1,000 sets per color configuration for forged aluminum or stainless steel sets. For custom die-cast molds requiring specialized tooling, initial order volumes can be tailored based on mold cost amortization agreements. Promotional or standard color runs may accept lower MOQs down to 500 units.
We source non-stick raw liquids exclusively from world-class chemical manufacturers (such as Whitford, ILAG, Chemours, and Greblon). Every chemical lot undergoes gas chromatography-mass spectrometry (GC-MS) testing before application, and full certification reports are provided for FDA and LFGB compliance prior to shipment.
High-tier 3-layer PTFE coatings offer superior long-term release capability (typically 3–5 years under standard domestic use and 35,000+ egg-cook cycles). Sol-Gel ceramic coatings provide extreme heat resistance up to 450°C without toxic fumes, delivering 1.5–3 years of peak non-stick performance depending on usage care and oil distribution.
Yes. We offer both full-cover impact-bonded stainless steel bases (SS430) and customized hole-pattern sprayed induction discs. Impact-bonded bases provide the highest induction response rate (heating up to 20% faster) and prevent thermal plate separation under extreme commercial kitchen usage.
For high-end premium cookware, total dry film thickness (DFT) is maintained between 35 to 45 microns ($\mu m$), comprising a 15–20 $\mu m$ primer, 10–15 $\mu m$ mid-coat, and 8–10 $\mu m$ topcoat. For standard retail lines, DFT ranges between 25 to 30 microns.
We offer ISTA 3A / 6-AMAZON ship-in-own-container (SIOC) certified mailer boxes reinforced with high-density EPE foam inserts, as well as luxury 5-ply color gift boxes with spot-UV finishing, woven handles, and modular nesting dividers designed to maximize retail shelf appeal.
All custom molds developed under paid ODM contracts remain the exclusive intellectual property of the buyer. We sign binding Non-Disclosure Agreements (NDAs) and non-compete covenants guaranteeing that proprietary mold shapes will not be offered to competing market distributors.
Initial orders requiring custom color matching, artwork approval, and packaging printing typically take 35–45 days. Repeat production orders are executed within 25–30 days. Rapid sample prototyping is completed within 7–10 days.
Our main export dispatches operate through Ningbo Port, Shanghai Port, and Shenzhen Port. We provide complete FOB, CIF, DDP, and EXW freight terms supported by automated container loading optimization to maximize CBM utilization.
Yes. All electric pressure cookers, multi-cookers, and commercial rice cookers hold complete certification packages including CE, CB, GS, UL, ETL, RoHS, and KC marks, guaranteeing smooth customs clearance across European, American, and Asian markets.
Elevate your cookware product line with precision metallurgy, advanced non-stick coating technology, and factory-direct B2B pricing. Contact our engineering and sourcing team today for instant quotes, technical drawings, and factory audit scheduling.